In most industries, sustainability is presented as a cost you accept for market access. In textile dyeing and finishing it is mostly the opposite. Water, heat and chemicals are purchased inputs, and the same interventions that reduce environmental load reduce the monthly bill.
Why cost and sustainability point the same way in dyeing
A dyeing and finishing mill buys water, heats it, doses it with chemistry, uses it briefly and then pays again to treat it before discharge. Every litre is paid for at least twice. Every degree of heat that leaves through an exhaust stack was paid for in gas or coal. Reducing consumption therefore shows up directly in overhead, and it does so every month rather than once.
This is why sustainability investment in this sector has a payback period that can be calculated rather than argued. The question is where the leaks are.
Leak one: water
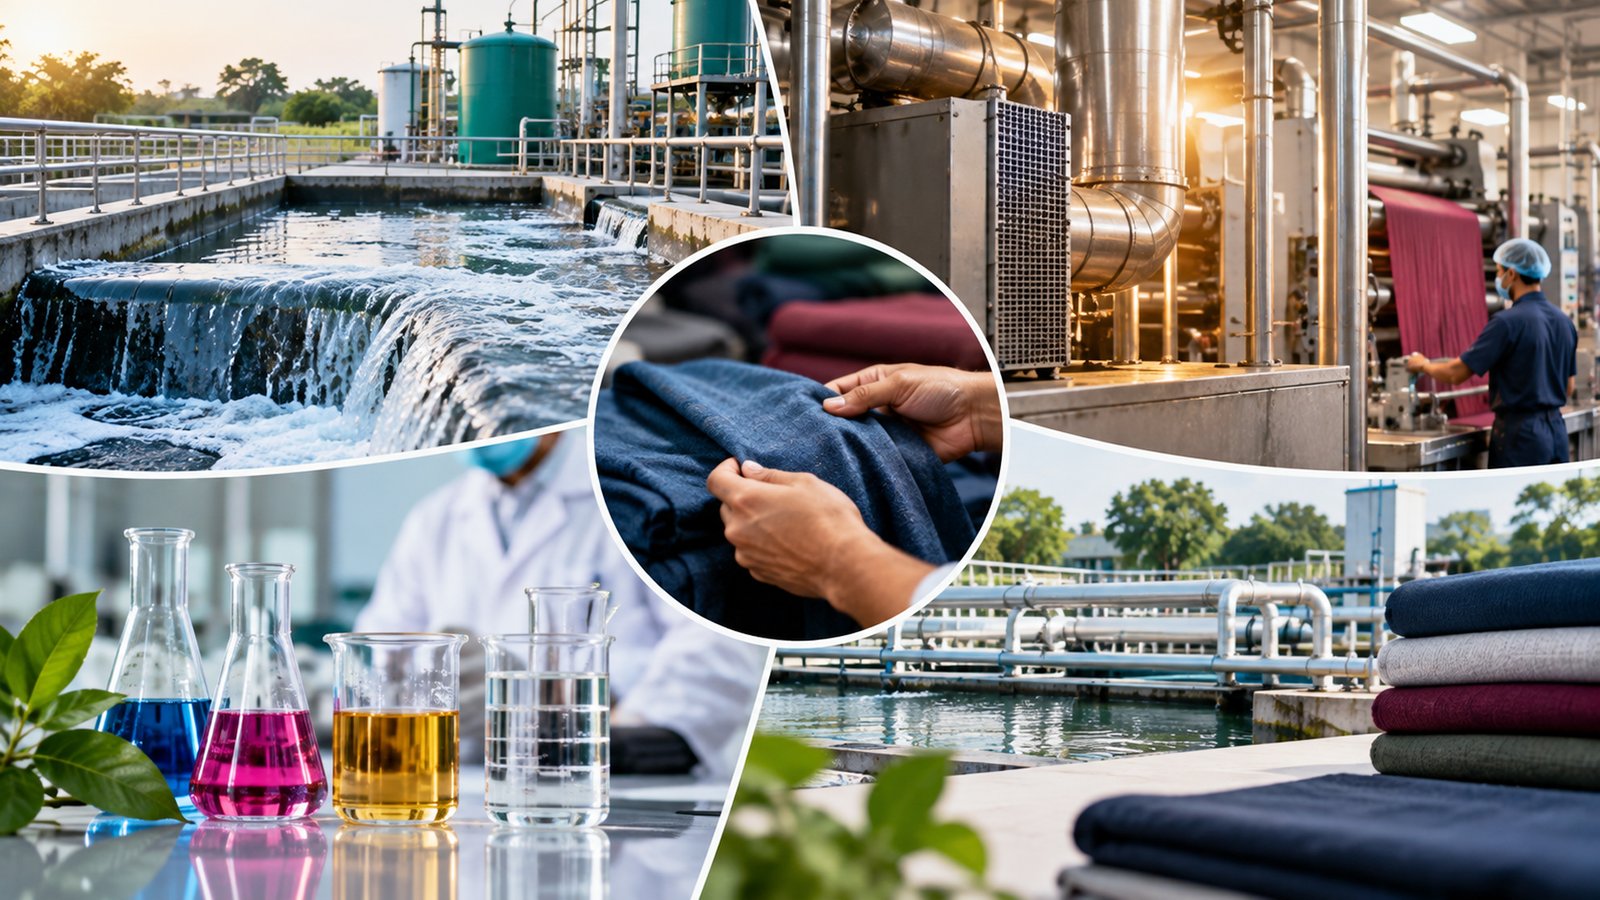
Water consumption in dyeing is driven by liquor ratio, machine selection, process recipe and rinse cycles. Mills that measure consumption per kilogram of fabric rather than per month usually find variation between shifts and machines that nobody had visibility of. Beyond process optimisation, treated effluent can be recovered and reused for selected applications, which reduces both intake volume and discharge volume. Whether reuse is viable depends on the treatment standard achieved and the process the recovered water re-enters.
Leak two: thermal energy
Heat is the input most often written off. Hot effluent leaves the dyeing machine, hot exhaust leaves the stenter, and both carry energy that was paid for at full price. Heat recovery systems capture part of that energy and return it to preheat incoming water or air. Colormatch BD represents German heat recovery technology for exactly this application, alongside its broader technical service to the industry.
The economics depend on running hours, temperature differential and existing utility cost, so the assessment has to be site-specific. A system that pays back quickly in a three-shift operation may not in a single-shift one.
Leak three: chemistry
Chemical selection affects far more than the chemical bill. It determines process time, wash-off requirement, water consumption, effluent load and, increasingly, whether a buyer will accept the goods. International brands have moved from testing finished garments to auditing the chemical inputs used in production, which pushes documentation requirements back to the chemical supplier.
The standards most frequently referenced include the ZDHC Manufacturing Restricted Substances List, OEKO-TEX certification for textile chemicals, and REACH requirements for goods entering the European Union. Verify the current version and scope of each directly with the issuing body, as they are revised regularly. Colormatch BD has worked with the Bangladeshi textile industry for close to three decades with sustainability as its stated focus.
Effluent is the last place to look, not the first
An effluent treatment plant is sized for the load it receives. Reducing water consumption and selecting cleaner chemistry lowers that load, which in turn lowers the capital and running cost of treatment. Mills that solve the discharge problem without touching the process end up paying to treat volume they never needed to generate. Charm Ltd., within the same group, installs effluent and water treatment plants for the textile, dyeing and finishing industry, which makes the process-side and treatment-side decisions easier to align.
Where to start
Measure first. Consumption per kilogram of production for water, steam and chemistry, broken down by machine and shift, tells you where the money goes. Most mills discover their largest single saving before they buy anything.
FAQ
How can a textile mill reduce water consumption in dyeing?
Through liquor ratio and recipe optimisation, machine selection, rinse cycle control, and recovery of treated effluent for selected reuse applications. Measuring consumption per kilogram of fabric by machine and shift usually exposes the largest savings before any equipment is purchased.
What is heat recovery in textile finishing?
Heat recovery captures thermal energy from hot effluent or exhaust air that would otherwise be discharged, and uses it to preheat incoming water or air. Payback depends on running hours, temperature differential and current utility cost, so it needs a site-specific assessment.
Why do garment buyers audit chemical suppliers?
Because testing a finished garment identifies a problem only after production is complete, when the cost of failure is highest. Controlling chemical inputs prevents restricted substances entering the process, which is why buyer requirements now reach back to the chemical supplier.
Does reducing water use lower effluent treatment cost?
Yes. A treatment plant is sized and operated for the load it receives, so reducing consumption and selecting cleaner chemistry lowers both the capital cost of the plant and its running cost.